
Vithy vs. Competitors: Why Vithy’s High-Quality Industrial Cartridge Filters Are the Superior Choice
Global Trends and Market Drivers in Industrial Filtration
The industrial filtration sector is experiencing tremendous growth, due to environmental policy, technological development and high-precision manufacturing processes. Furthermore, with increasingly stringent regulatory frameworks regarding industrial discharge becoming a primary operational requirement for industries, filtration has moved from being secondary utility to becoming an essential operational need.
Current market dynamics show that the growth of semiconductor, lithium-ion battery and biopharmaceutical industries has significantly altered filtration requirements. These industries operate under cleanroom conditions where trace contaminants cause significant production losses; electronic-grade chemical production requires removal of particles as small as 0.1 micrometers to ensure reliable microcircuit operation; this demand for extreme precision has forced a shift in market trends, placing greater value on manufacturers with absolute-rated media and verified retention capabilities.
Filtration technology has become a key enabler of corporate sustainability strategies. Filtration filtration enables circular economies, helping companies reuse process water, recover catalysts and reduce waste. Today's systems are evaluated on their ability to conserve both water and energy usage. High-flow cartridge systems with more filter surface area in a smaller footprint have become the go-to choice for plants looking to optimize utility consumption while still meeting high throughput needs; their focus on resource efficiency fuels innovation in filter longevity as well as cleanable, reusable media development.
Material Science in Cartridge Development
An industrial cartridge's performance is determined by its media composition and structural design. Modern industry requires an expansive material palette capable of withstanding various chemical and thermal stresses:
Polymeric Media: Vithy's melt-blown cartridges feature polypropylene (PP), PES and PTFE materials to provide chemical compatibility across a wide pH range, while inner layers provide final polishing to eliminate premature surface blinding while increasing filter capacity to decrease operational downtime. This design prevents premature surface blinding while simultaneously optimizing operational uptime by holding more contaminants within its depths than ever before.
Sintered Metal Technology:
Vithy's UHMWPE/PA/PTFE powder sintered cartridge are more rigid and less prone to deformation compared to foam, especially when exposed to acceptable temperatures. Even if the filter cake on the outer surface of the filter cartridge is viscous, it can be easily separated by blowing back with compressed air. In addition, after blowing back the filter cake with compressed air, the high-speed air is squeezed out of the pores, and the solid particles captured during the filtration process are discharged by using kinetic energy. It makes it convenient to remove cake and regenerate the filter cartridge, and reduces the labor intensity of the operator. The UHMWPE/PA/PTFE filter cartridge demonstrates strong resistance to various chemicals such as acid, alkali, aldehyde, aliphatic, hydrocarbons, and radioactive carbon. It can also withstand ester ketones, ethers, and organic solvents below 80℃ (PA up to 110℃, PTFE up to 160℃).
For high-temperature and high-pressure environments, sintered metal cartridges offer an effective solution. Constructed from either 316L stainless steel or titanium powder, these components can withstand temperatures reaching 600degC while still remaining resistant to solvents that degrade synthetic fibers.
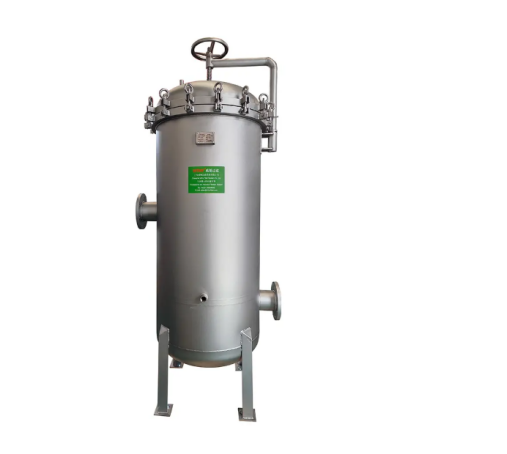
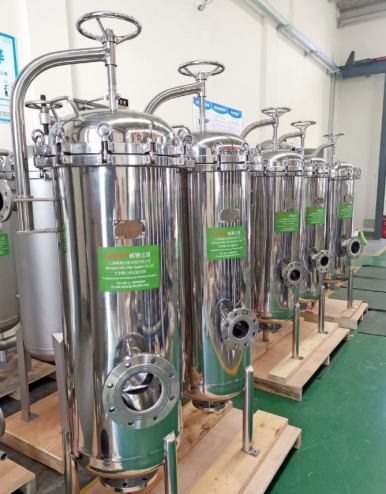
High-Flow Configurations: As plant capacities have grown, industry has increasingly turned toward high-flow pleated cartridges for their increased filtration area and smaller housing footprint. These designs use special pleat geometry to increase effective filtration area allowing one cartridge to handle flow rates previously covered by multiple standard filters resulting in shorter maintenance intervals and quicker repairs.
Engineering and Structural Integrity
Beyond media, structural components like core, cage, and end caps must also be designed to prevent bypass. High-quality systems utilize thermal bonding techniques rather than adhesives to affix these parts together to the filter element - this guarantees no chemical extractables enter the fluid stream. A rigid outer cage is particularly crucial in applications with fluctuating pressures because it prevents pleats collapsing while upholding seal integrity over its service life.
Application Profiles and Industry Adoption
Cartridge filtration can easily integrate into diverse process flows across several major sectors, and has proven its efficacy by being consistently applied in high-stakes environments.
Chemical and Petrochemical Processing
Filtration systems play a crucial role in chemical manufacturing. Filter systems help purify raw materials, protect catalysts from degradation, and ensure final product purity. Cartridge filters often serve as final "police" filters before packaging to maintain standard for specialty chemicals; companies often select high-quality systems capable of withstanding corrosion-inducing fluids while upholding precise micron ratings to meet these specifications.
Food and Beverage Production
Filtration systems used in food production must adhere to stringent food-grade standards, effectively eliminating spoilage organisms without impacting flavor or nutritional profiles. Common applications for this process are edible oils, liquid sugars and dairy products.
New Energy and Battery Materials
Producing lithium-ion batteries involves dealing with viscous slurries and acidic electrolytes. Filtration plays an integral part in purifying lithium salts and creating electrode materials, while special cartridges with precision micron ratings ensure the highest yield and safety ratings in final battery cells.
Heavy Industry and Resource Management
Filtration systems play a pivotal role in managing cooling water and process fluids for steel and paper industries. By filtering out scale and debris from recycled water sources, filter systems protect spray nozzles and heat exchangers from becoming blocked up with scale deposits that could clog.
Implementation Impact and Global Client Integration
Adopting high-quality filtration can have a measurable effect on total cost of ownership. In pharmaceutical settings, steam-sterilizable sintered titanium filters allow repeated use in sterile environments without waste from disposable units.
These technologies reach across the world through an expansive network of technical support and distribution that spans Europe, Russia, Middle East, Southeast Asia and Americas. This ensures industrial operators have access to technical expertise required for selecting appropriate media and housing configurations for their production environments. Shanghai Vithy Filter System Co. Ltd has over 15 years of core team experience to tailor every installation according to each individual client's production environment.
Conclusion
Industrial filtration has evolved from being an essential utility into a strategic asset that influences production quality, environmental compliance and operational efficiency. As manufacturing processes become more sophisticated, demand for reliable separation technology increases exponentially. Shanghai Vithy Filter System Co. Ltd. remains at the forefront by emphasizing material science, structural engineering and application-specific design. By offering solutions that meet the stringent standards set forth by global industry leaders across chemical, food, energy, and pharmaceutical sectors, this company underscores the significance of meticulous filtration in modern industrial era. With their commitment to research coupled with superior manufacturing standards and over 30 patents under their belts, these systems meet up with an increasingly challenging global market.
For further technical information on industrial filtration systems and their applications, visit the official website: https://www.vithyfiltration.com/
Shanghai Vithy Filter System Co., Ltd.
Shanghai Vithy Filter System Co., Ltd.
email us here
Legal Disclaimer:
EIN Presswire provides this news content "as is" without warranty of any kind. We do not accept any responsibility or liability for the accuracy, content, images, videos, licenses, completeness, legality, or reliability of the information contained in this article. If you have any complaints or copyright issues related to this article, kindly contact the author above.
